Medical-Grade Plastics CNC Machining: Precision Guide
Medical-Grade Plastics CNC Machining: Engineering Integrity for Critical Applications
Machining engineering polymers for biomedical devices demands an entirely different paradigm than cutting metals. Polymers exhibit high coefficients of thermal expansion (CTE), low thermal conductivity, viscoelastic recovery, and vulnerability to chemical leaching.
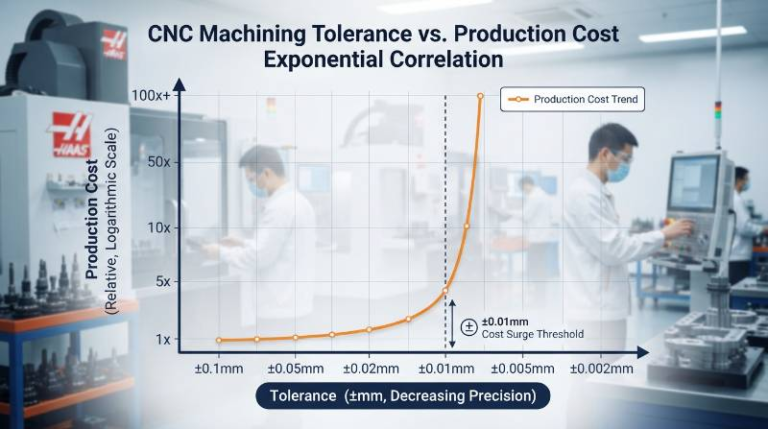
Standard machining approaches routinely cause internal residual stresses, micro-cracking during autoclave cycles, and lot-level biocompatibility failures. In mission-critical surgical devices and implant trial systems, dimensional drift of even 15 μm can compromise fluidic seals or kinematic alignments.
Precision medical device engineering relies heavily on strict compliance frameworks, requiring parts built for regulated medical manufacturing industries to adhere to rigorous ISO 13485 alignment, USP Class VI resin certifications, and zero-hydrocarbon cleanroom protocols from rough cutting through final verification.
Engineering Evaluation Matrix: The 4 Critical Dimensions of Precision Medical Plastic Machining
To ensure consistent quality across production batches, manufacturing engineers evaluate polymer component fabrication across four technical axes:
Evaluation Framework: A rigorous methodology scoring Material Traceability, CTE Compensation, Coolant Chemistry, and Metrological Stability at 20°C before initiating production cuts.
- 1. Material Certification & Lot Traceability: Complete physical and chemical certs matching ASTM and ISO 10993 cytotoxicity standards. Raw stock must be 100% resin-certified with zero regrind or unapproved additives.
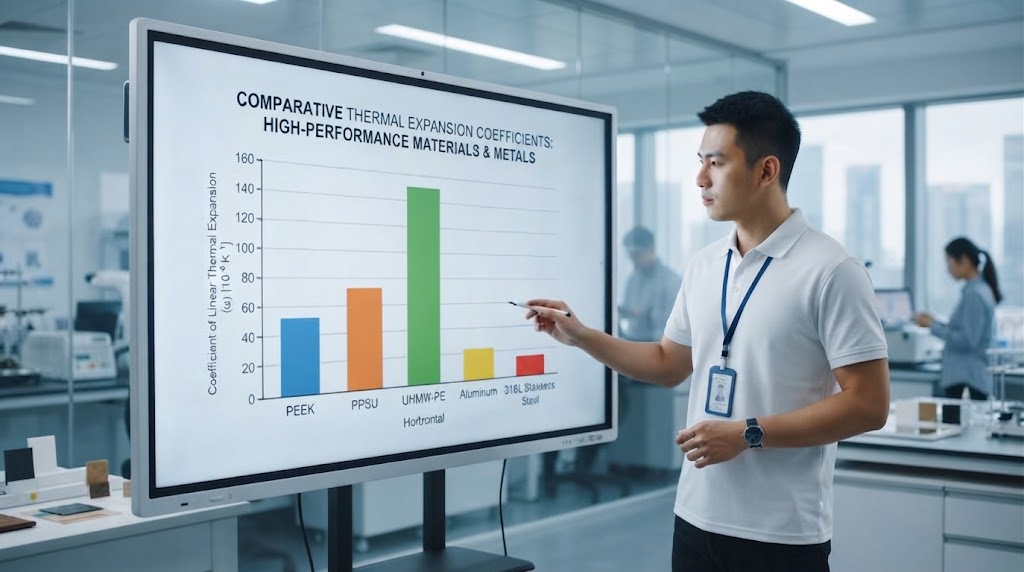
- 2. Thermal Management & CTE Compensation: Medical plastics expand at rates up to 10× that of structural metals. Real-time tool-path thermal compensation prevents localized heat build-up and tool-induced plasticization.
- 3. Contamination Control & Coolant Chemistry: Eliminating standard mineral oil-based cutting fluids prevents polymer swelling and hydrocarbon absorption. Dry machining, pure vortex cold air, or USP purified deionized (DI) water mist are required.
- 4. Geometric Stability & Metrology: Contact and optical coordinate metrology must occur in a temperature-controlled environment at 20°C ± 0.5°C following minimum 24-hour part stabilization.
Medical Polymer Selection Guide: Mechanical, Chemical, and Biocompatibility Profiles
Selecting the right polymer requires balancing mechanical yield strength against chemical exposure, sterilization durability, and machinability characteristics. Sourcing fully traceable, certified medical-grade materials ensures zero baseline biological contamination.
| Polymer (Trade Name) | Tensile Strength (MPa) | CTE (10⁻⁵ / K) | Max Service Temp (°C) | Primary Machining Challenge |
|---|---|---|---|---|
| PEEK (Optima / TECAPEEK) | 95 – 110 | 4.5 – 5.0 | 250 | High cutting resistance; severe residual stress cracking if unannealed. |
| PPSU (Radel) | 70 – 80 | 5.5 – 6.0 | 180 | Notch sensitivity; micro-crazing at tool exit edges. |
| PEI (Ultem 1000) | 100 – 115 | 5.0 – 5.5 | 170 | Brittle chip formation; prone to micro-cracking under dull tooling. |
| UHMW-PE (GUR 1020) | 25 – 40 | 15.0 – 20.0 | 90 | Extremely ductile; elastic recovery leads to severe burr formation. |
| PTFE (Teflon) | 20 – 35 | 12.0 – 16.0 | 260 | Continuous creep; highly prone to clamping deformation. |
| POM-C (Medical Acetal) | 65 – 75 | 10.0 – 12.0 | 100 | Moderate thermal expansion; centerline porosity in thick blocks. |
Sterilization Compatibility Matrix: Autoclave, EtO, Gamma, and Plasma Resistance
Medical instruments undergo repetitive sterilization protocols. Unrelieved internal stresses introduced during CNC roughing accelerate Environmental Stress Cracking (ESC) when exposed to high-temperature steam or chemical sterilants.
| Polymer | Steam Autoclave (134°C) | Ethylene Oxide (EtO) | Gamma Irradiation (50 kGy) | VHP Plasma (STERRAD) |
|---|---|---|---|---|
| PEEK | Excellent (>1,000 cycles) | Excellent | Excellent | Excellent |
| PPSU | Excellent (>1,000 cycles) | Excellent | Moderate (Color shift) | Excellent |
| PEI | Good (≈100-150 cycles) | Excellent | Good | Moderate |
| UHMW-PE | Poor (Deforms >90°C) | Excellent | Requires Cross-linking control | Good |
| POM-C | Moderate (20-30 cycles) | Excellent | Poor (Chain scission) | Poor |
The Tyneen Multi-Stage Stress-Relief Annealing Protocol™ (MSRAP)
Semi-crystalline and amorphous medical plastics store significant internal kinetic stresses during extrusion and heavy machining. Without proper thermal normalization, components warp during finishing passes or fail in sterilization autoclaves.
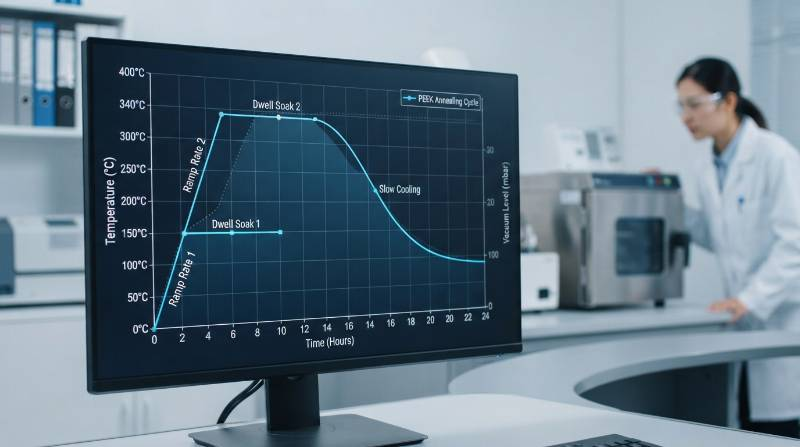
To guarantee ±0.005 mm precision across complex geometries, Tyneen applies an automated 4-stage vacuum thermal cycle:
- Raw Stock Normalization: Stock billets are heated in a vacuum furnace to 200°C (for PEEK) at a ramp rate of 10°C/hour to relieve baseline extrusion stresses.
- Roughing Stage De-stress: After rough milling leaves 0.50 mm of uniform stock allowance, parts undergo a secondary intermediate thermal dwell at 160°C to release bulk cutting strains.
- Semi-Finishing Soak: Post semi-finishing (leaving 0.05 mm allowance), parts undergo an isothermal equalization soak to stabilize crystalline grain alignment.
- Controlled Slow Cooling: The furnace slowly cools at ≤ 5°C/hour to room temperature, preventing the formation of skin-core thermal gradients.
Contamination-Free Machining: Oil-Free Coolant & Cryogenic Deflashing Strategies
Standard cutting oils can leach into porous polymer matrices, violating ISO 10993-5 cytotoxicity standards. Tyneen isolates medical plastics across specialized clean CNC cells.
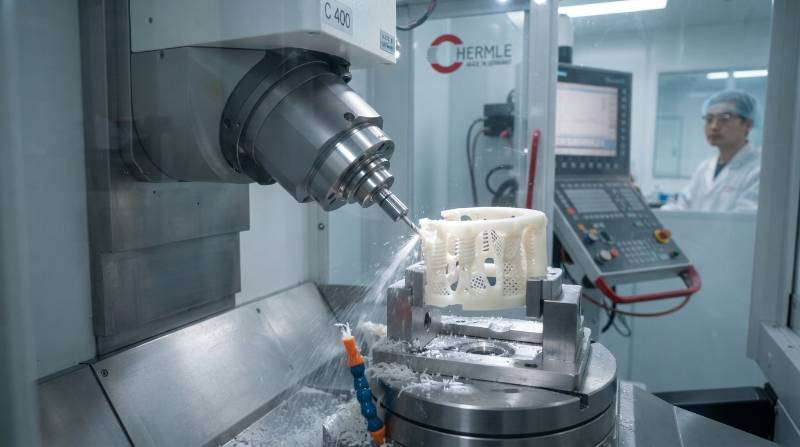
We eliminate hydrocarbon contamination using filtered vortex cold air guns (-40°C air stream) or closed-loop USP Grade Purified DI Water mist. For complex micro features, our 5-axis advanced machining centers maintain clean chip evacuation without chemical coolants.
For ductile polymers like UHMW-PE and PTFE that tend to smear rather than shear crisply, we apply liquid nitrogen cryogenic deflashing. Cooling flash edges past their glass transition temperature (Tg) allows non-abrasive micro-media tumbling to cleanly fracture burrs without altering critical bore tolerances.
Vc: Cutting Speed (m/min), D: Tool Diameter (mm), n: Spindle Speed (RPM). For unreinforced PEEK, maintain Vc = 150 – 250 m/min with high chip load to prevent localized frictional melting.
High-Complexity Case: 5-Axis Micro-Machining of PEEK & PPSU Surgical Robotics Fluidic Manifolds
A leading minimally invasive surgical robotics OEM required a high-density hydraulic distribution manifold made from unfilled virgin PEEK (TECAPEEK MT).
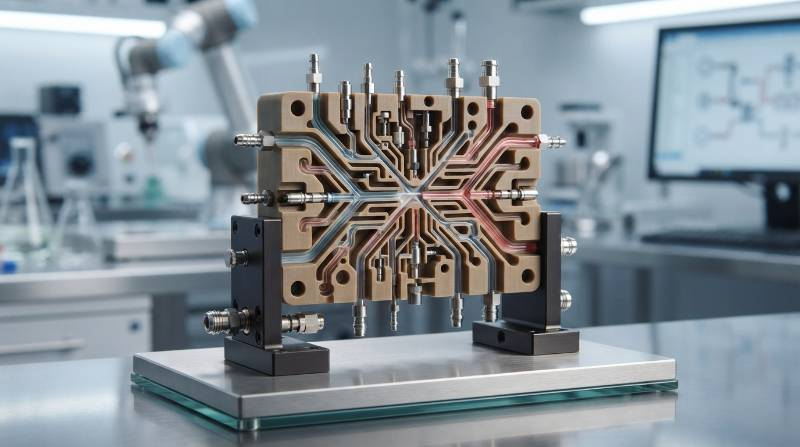
- Geometry & Challenge: 24 internal intersected fluidic ports measuring ⌀0.8 mm across a 60 × 40 × 30 mm block, with zero internal burrs permitted and a bore location tolerance of ±0.008 mm.
- Tooling Solution: Single-crystal diamond (PCD) micro end mills with single-flute geometries, cutting dry with -40°C compressed air cooling on our precision CNC milling services lines.
- Thermal Control: Multi-pass stepped clearing with the Tyneen MSRAP thermal protocol between roughing and finish boring.
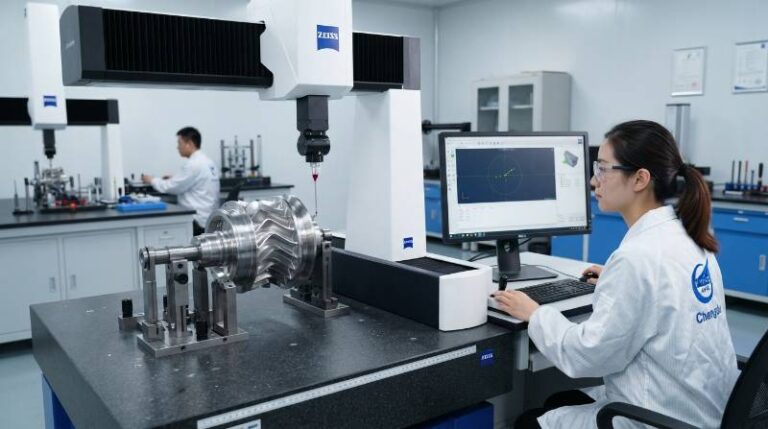
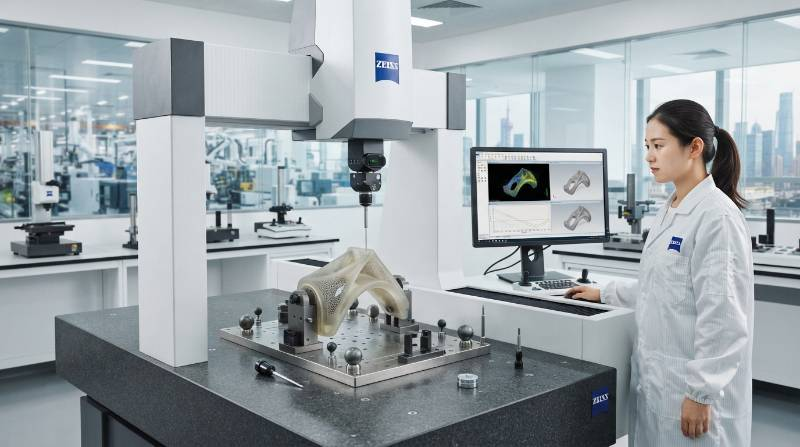
- Inspection & Verification: Internal cross-holes inspected via micro-borescopes and verified on a Zeiss CMM, confirming true position bore locations within 0.006 mm and Ra 0.35 μm surface finishes.
Tyneen Medical Machining Capabilities: Climate-Controlled Facilities & Quality Assurance Standards
To eliminate thermal drift during micro-milling and turning operations, Tyneen operates climate-controlled machining bays maintained strictly at 20°C ± 0.5°C with 45% relative humidity.
Our quality management infrastructure is certified to ISO 9001:2015, IATF 16949, and AS9100D, fully supporting client compliance requirements under ISO 13485:2016. Tight-tolerance cylindrical components are produced using our specialized high-precision CNC turning centers.
| Capability Metric | Tyneen Production Standard | Verification Equipment / Process |
|---|---|---|
| Milling Tolerances | ±0.005 mm (±0.0002 in) | 5-Axis DMG MORI High-Precision Centers |
| Turning Tolerances | ±0.003 mm (±0.00012 in) | Swiss-Type Lathes with Live Tooling |
| Surface Finish | Ra 0.2 μm to Ra 0.4 μm | Non-contact White Light Interferometry |
| CMM Metrology | Volumetric accuracy 0.9 μm + L/350 | Zeiss PRISMO / O-INSPECT Multisensor |
| Contamination Control | Class 7 Cleanroom Cleaning & Packing | Multi-stage Ultrasonic DI Wash Lines |
Deep Material & Process Comparisons: PEEK vs Metals and Machining vs 3D Printing
PEEK vs Titanium Grade 5 (Ti-6Al-4V): Biomechanical & Radiopacity Trade-offs
PEEK offers an elastic modulus (≈3.6 GPa unfilled, up to 18 GPa carbon-reinforced) that closely matches human cortical bone (≈18 GPa), drastically reducing stress shielding compared to Titanium Grade 5 (≈110 GPa).
Additionally, PEEK is radiolucent, allowing artifact-free X-ray and CT imaging of bone growth during postoperative recovery. Titanium remains the material of choice for high-load joint replacements, but PEEK excels in spinal fusion cages and neurosurgical implants.
CNC Machining vs 3D Printing (SLS/FDM) for Medical PEEK Prototypes
Additive manufacturing methods like FDM and SLS for PEEK frequently suffer from inter-layer delamination, internal micro-porosities, and anisotropic tensile loss (Z-axis strength drops of 30-50%).
Subtractive 5-axis CNC machining uses continuous-extruded, solid stock shapes certified to ASTM F2026. This guarantees fully isotropic mechanical strength, a pore-free internal matrix, and mirror surface finishes (Ra < 0.4 μm) required for dynamic blood-contact surfaces.
3-Step Production Pathway: Fast-Track Your Precision Medical Components with Tyneen
Transition from prototype to commercial validation through Tyneen’s verified medical plastics workflow:
Fast-Track Medical Manufacturing Pathway
- Step 1: Upload CAD & Requirements — Submit your 3D STEP/IGES models along with GD&T specifications and resin cert requirements.
- Step 2: Automated DFM & Engineering Review — Receive a complete manufacturability report, tooling breakdown, and firm quote within 2 hours.
- Step 3: Rapid Production & Inspection — Precision 5-axis machining with intermediate vacuum annealing, complete Zeiss CMM inspection reports, and worldwide clean-packaged dispatch.
Frequently Asked Questions on Medical-Grade Plastics CNC Machining
How do you prevent burrs in ductile plastics like UHMW-PE?
We use razor-sharp single-crystal diamond (PCD) tools with polished positive rakes (>15°), combined with high cutting speeds and liquid nitrogen cryogenic deflashing after machining.
Can you machine medical plastics without coolant?
Yes. We use -40°C vortex cold-air guns or USP-purified DI water mist to prevent localized heating while avoiding hydrocarbon coolant absorption.
How is lot traceability managed for implant-grade materials?
Every raw billet is tagged with melt batch certificates conforming to ASTM F2026 or USP Class VI, tracked through internal ERP routing, and documented in First Article Inspection (FAI) reports.
What is the typical turnaround time for custom medical plastic prototypes?
Prototype quantities with complete FAI and material certification typically ship in 3 to 7 business days, supported by our 2-hour DFM engineering review.